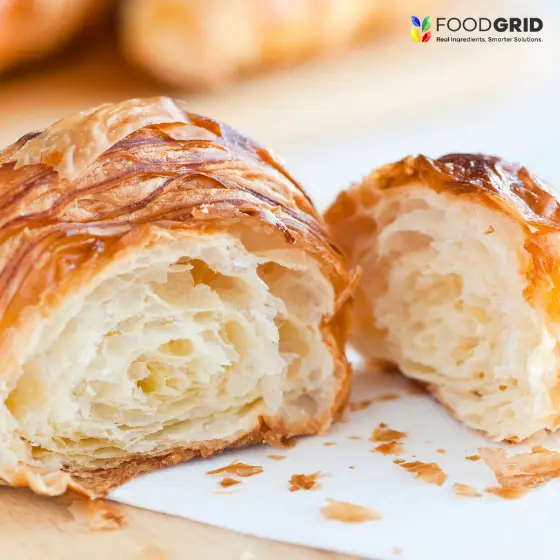
Your lamination line ran clean in the pilot trial. Consistent layers, good lift, no fat bleed. Then you scaled up, or doubled throughput, or summer arrived, and the results changed.
The dough started tearing at the sheeter. Fat smeared into the dough instead of staying in distinct layers. Lift dropped. A product that tested perfectly at small scale started varying from batch to batch.
The root cause is almost always the same: the margarine was qualified under conditions that don’t match your real production environment. It performed in development. It doesn’t perform at your actual temperatures, throughput, and mechanical load.
This post covers the spec numbers that only reveal problems at commercial scale, and what to confirm with your supplier before you commit.
Why Scale Changes Everything
A 10 kg trial behaves differently from a 300 kg-per-hour line, for physical reasons.
At small scale, you control fat and dough temperatures closely. The sheeter runs slowly, the fat has time to settle between folds, and the room temperature stays steady.
At commercial scale, the sheeter runs continuously. Roller friction warms both the dough and the fat. Floor temperature drifts over a shift, especially without precise climate control. Rest times between folds shorten. The fat is under more mechanical stress for longer than any pilot can reproduce.
Those conditions expose weaknesses a trial hides. A fat with a narrow working range holds up at low speed and breaks down at high speed. A fat that’s fine on a cool morning bleeds by midafternoon. A fat that loses solidity too quickly as it warms smears at the fold instead of sheeting cleanly.
The most common failure is a mismatch between fat and dough firmness. If the dough is softer than the fat, the fat breaks through. If the fat is softer than the dough, it smears into the layers. Both produce unusable product, and both trace back to a spec that wasn’t checked against your real conditions.
Number One: Slip Melting Point
Slip melting point is where the fat shifts from something that sheets cleanly to something that smears. It’s your first indicator of how the fat will behave as the floor warms up through a shift.
Puff pastry margarines typically have higher slip melting points than croissant margarines. Puff grades often run around 40–47°C (104–117°F), and croissant grades around 32–40°C (90–104°F) [VERIFY both ranges against FoodGrid’s specs]. The right value for you depends on your floor temperature, oven entry temperature, and how long the dough sits on the line.
If the slip melting point is too close to your working temperatures, your window is narrow. The fat handles well at the start of a cool shift, softens as the room warms, and by the end of a long run your lamination quality has drifted.
That drift can’t be fixed at the sheeter. It’s a spec problem, solved before the order is placed. Ask your supplier for a specific slip melting point with a documented tolerance, not a broad range, and test at the warmest point of your shift over a full production run.

Number Two: The Solid Fat Content Curve
Slip melting point tells you when the fat gets too soft. The solid fat content (SFC) curve tells you how it behaves at every temperature in between. You need both, and for predicting real performance on a variable line, the curve tells you more.
SFC is the percentage of fat that’s still solid at a given temperature. The shape of the curve matters more than any single point:
- A steep curve means the fat loses solidity quickly with small temperature changes. It handles precisely at your target and fails fast if the line runs warm.
- A gradual curve gives a wider working range that tolerates temperature swings.
Two fats with the same slip melting point can behave very differently on the line if their curves differ. For a line without tight temperature control, a gradual curve is the safer choice. A good laminating margarine also keeps enough solid structure into the early bake for the layers to set before the fat melts out.
Ask for SFC values at a minimum of 10, 20, 30, and 35°C (50, 68, 86, and 95°F). A spec sheet with only a melting point doesn’t give you the curve.
FoodGrid’s Puff Pastry Margarine is engineered with a controlled SFC profile and a natural butter flavor system, is trans fat-free, and comes with full SFC data at onboarding.
Number Three: Plasticity Range
Plasticity is the temperature band where the fat bends and sheets without cracking (too cold) or smearing (too warm). On a pilot line, you can work within a narrow band. On a commercial line, a narrow band means constant adjustment.
One of the main advantages of a roll-in margarine over butter is a wider, warmer working window. Butter typically needs to stay around 13–16°C (55–61°F) for roll-in, while roll-in margarines are designed to stay workable at warmer temperatures [VERIFY: insert FoodGrid’s documented plasticity range and recommended working temperature here]. For facilities where the temperature rises across a shift or a season, that extra margin can prevent failures without new equipment.
The check that matters: make sure the top of the documented plasticity range sits comfortably above your floor temperature at its warmest point in the day, not just your start-of-shift target. A fat whose range ends just above your morning temperature will fail in the afternoon.
For procurement, get the plasticity range in writing. A supplier who can give only a target working temperature, without a range, can’t support you in a quality dispute.
Number Four: Water Content
Water in a laminating fat turns to steam in the oven and pushes the layers apart, which is part of what gives puff pastry and croissants their lift. Too little water means less steam and less lift. Too much can cause bleeding on the line [VERIFY other effects with R&D].
At commercial scale, the issue isn’t that a given variance matters more per piece. It’s that you go through far more lots. Lot-to-lot variation that barely registers over a few pilot runs shows up as real day-to-day inconsistency when you’re running multiple lots a week.
So ask for a nominal water content plus the acceptable lot-to-lot variance. That range becomes your incoming inspection criterion, and any lot outside it gets flagged before it reaches the line. Water content should appear on the COA for every lot as standard, not on request.
The Documentation Checklist
Before the first order ships, your QA team should have:
- COA per lot, covering slip melting point, water content, free fatty acids, peroxide value, and SFC at key temperatures.
- The full SFC curve at 10, 20, 30, and 35°C minimum.
- Documented plasticity range, so production can set parameters and QA can set pass/fail criteria.
- Water content with acceptable variance.
- Allergen statements at product and facility level.
- Trans fat status in writing.
- RSPO certification status for palm-derived margarines.
- Confirmed lead times for your volume and production calendar.
FoodGrid provides all of these at onboarding. Review the qualification process at foodgridinc.com/purchasing.
The Supplier Behind the Spec Sheet
A spec sheet describes a fat under controlled conditions. A good supplier does more: confirms lead times before your production window, tells you when a lot is near the edge of spec, and supports your QA team when a retail buyer asks for an audit.
For multi-season supply agreements, those behaviors are worth as much as the fat itself. Before the first order, ask how the supplier handles a lot that tests at the edge of specification. The answer tells you whether you’re getting a partner or a commodity vendor.
Request Samples and Documentation
FoodGrid supplies puff pastry margarine and bulk bakery margarine for commercial laminated dough programs at retail, foodservice, and industrial scale, with full technical documentation ready before your first order.
Whether you’re qualifying a new supplier, troubleshooting a lamination failure, or building a new spec, contact our ingredient team or review the full puff pastry margarine specification at foodgridinc.com.
Real Ingredients. Smarter Solutions.


